
Purlin Roll Forming Machine
C and Z purlin machines for steel structure workshops — manual, quick-change or fully automatic.
Price range: C/Z purlin roll forming machines
US$39,000–62,000 (standard) · US$72,000–143,000 (premium), FOB China
Standard covers the first two configuration levels (single-profile and multi-profile / quick-change); premium covers fully automatic lines.
Final price depends on profile, thickness, speed, punching and automation. Excludes freight, import duties and installation. Send your profile drawing for a quotation within 24 hours. North American configurations (480V/60Hz, UL and local requirements) are quoted separately.
Large complete lines (e.g. truck chassis beam lines or full cable tray lines) are quoted per project, typically above US$150,000.
Manufactured in our Xiamen factory · 35+ years of roll forming experience.
Get a quote for this machine
Send your profile drawing or a photo of the profile. We reply within 24 hours with a configuration and price.
Commercial terms
- Lead time
- standard machines 30–60 days; automatic and heavy-duty lines 60–120 days (confirmed in the quotation).
- Warranty
- 12 months on the machine, lifetime technical support by video and remote guidance; wear parts excluded.
- Payment
- 30% deposit; 70% before shipment, after you approve the trial-run video.
- Shipping
- FOB Xiamen, China.
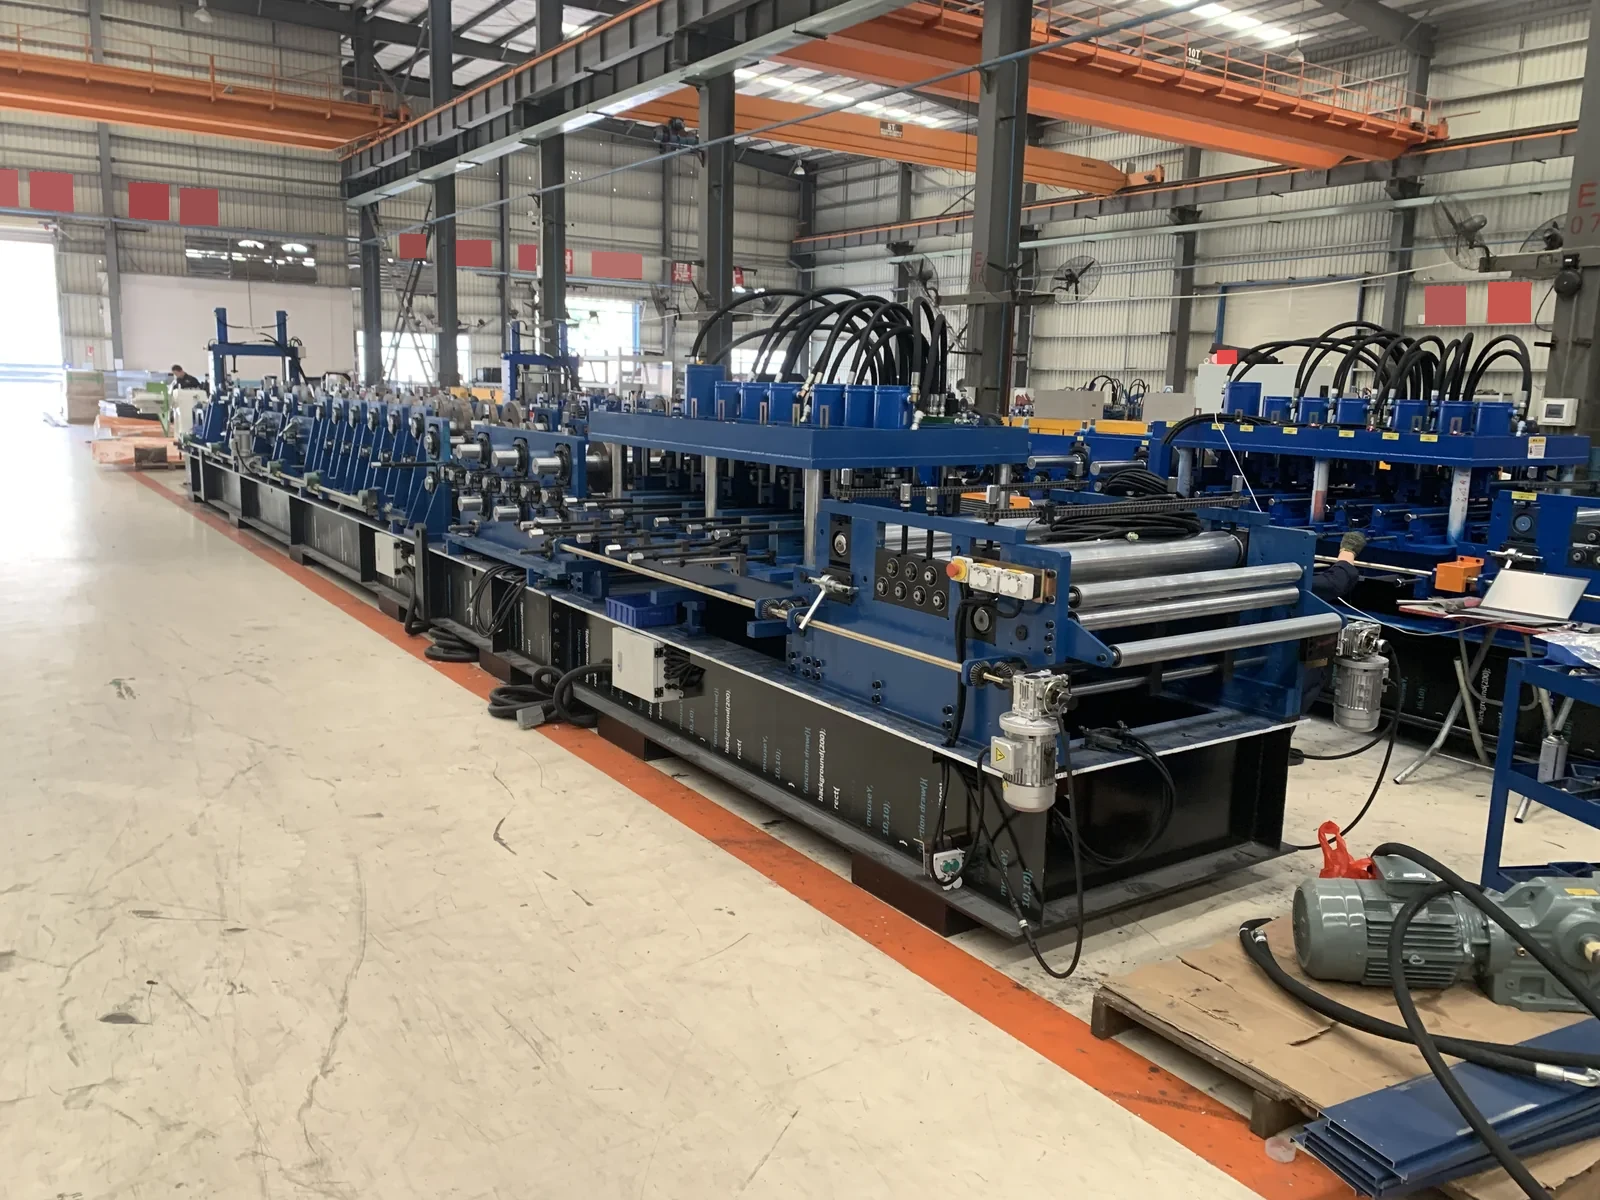
Which purlin roll forming machine fits your order mix?
Direct answer: Choose between a dedicated fixed-section line, a manually adjusted line and an automatic C/Z line using your real production schedule. The right choice depends on the number of section changes, the drawings and material, hole patterns, acceptable setup scrap and the output you need after each change. We confirm changeover time and speed for your own drawings in the quotation.
| Approach | Best question to ask | Evidence to compare |
|---|---|---|
| Fixed-section line | Will one approved profile dominate the production schedule? | Drawing and material range, sample dimensions, operating cycle for that section |
| Manual adjustment | How many adjustments and test parts are needed when changing size? | Recorded operator steps, setup time definition, first acceptable part and scrap |
| Automatic C/Z | Which axes and operations change from the recipe, and which still need an operator? | Two-profile trial in both directions, hole alignment, samples and measured output |
Watch one C/Z size-adjustment example
This public Halcyon HCZ-S20 workshop clip shows a production-base machine and explains what to ask about size adjustment. It does not show a timed C-to-Z changeover, measured trial parts or acceptance results for your order. Compare the proposed tooling and first acceptable parts against both approved drawings.
Check a published model range against your C and Z drawings
For one production-base catalogue example, HCZ-F5 lists C-section webs of 80–350 mm, Z-section webs of 120–350 mm, flanges up to 100 mm, lips up to 25 mm and material thickness of 1.0–3.5 mm. Compare the full profile geometry, steel grade and thickness together: an individual maximum does not mean every maximum can be combined in one approved section. These figures describe our Xiamen production base's published HCZ-F5 reference, checked 28 September 2026; they are not a specification or availability guarantee for every Halcyon offer. Request the named machine configuration and trial parts for the smallest and largest drawings before approving a quotation.
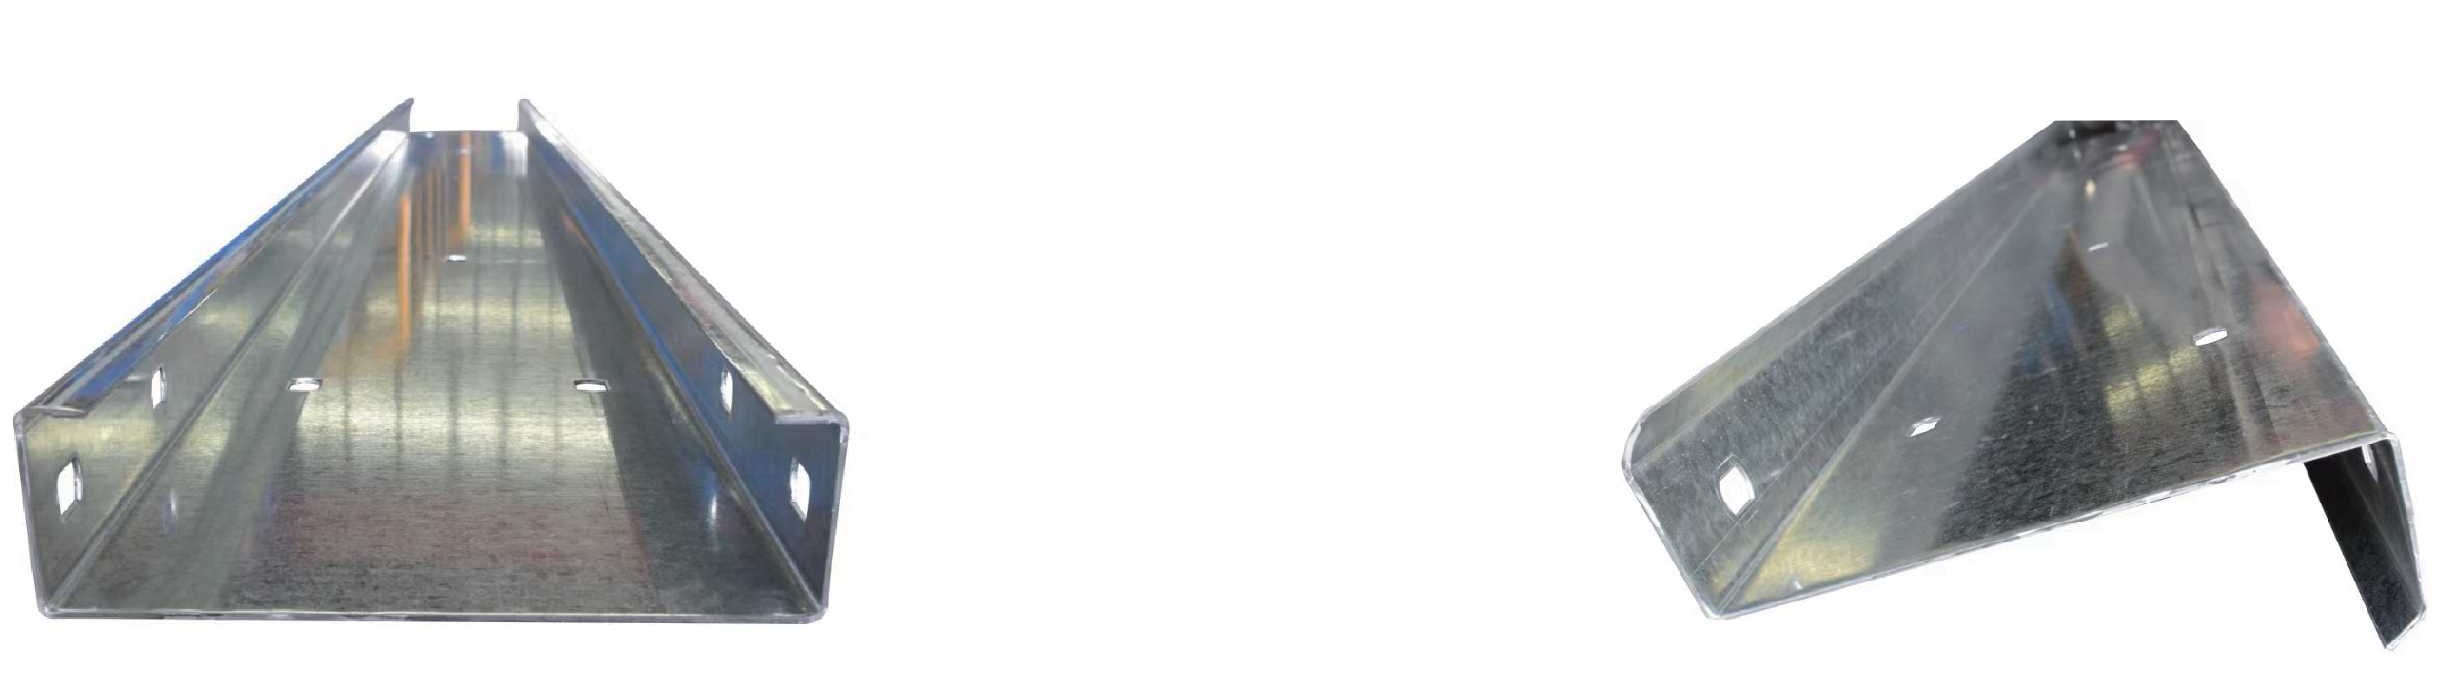
Pre-punching or post-punching: which process matches your purlin drawing?
Direct answer: Neither punching position is universally better. The buyer needs to know whether holes and slots are made in the flat strip before forming or in the formed C/Z section afterward, then check the finished part against the same approved hole-layout drawing. The quoted tooling, cut sequence and trial material matter more than the process label alone.
| Published process example | What to confirm in the offered line | Trial record to request |
|---|---|---|
| Pre-punching: NL300 lists punching and pre-cutting before roll forming. | Which holes and slots are punched in the flat strip, and which drawing dimensions control their final positions after forming? | Identify the trial coil and drawing revision; measure finished hole centres, edge distances and cut lengths on C and Z samples. |
| Post-punching: HCZ-450F lists forming before its post-punching station. | Which hole patterns, dies and adjustments are included for both formed sections? | Measure the same features on finished C and Z samples and record the actual punching and cutting cycle. |
Source: NL300 published process and HCZ-450F published process, checked 28 September 2026. These are production-base reference models; the route, tooling set and tolerance for your line are stated in the signed machine specification and confirmed with witnessed samples.
Browse purlin machines by the profiles you need
Use the required section drawings to narrow the machine family before comparing price or speed. Each linked page explains a different equipment scope; the final tooling and capacity still depend on the quoted build.
- Both C and Z sectionsAutomatic C/Z purlin roll forming machines — compare included adjustments, punching and two-direction changeover.
- Only Z sectionsZ purlin roll forming machine — check the approved Z drawing, lap-hole positions and sample fit.
- C-only line selectionC purlin roll forming machine guide — compare fixed C, adjustable C and the C/Z alternative by your approved drawing.
- Small C sectionsM Series C-section forming machine — review the published model family against your C drawing and production mix.
- L Series C or C/Z variantsCompare HC-300L C-only and HCZ-300L C/Z references — historical variant names guide questions, but current tooling and availability require a model-specific proposal and trial.
For the wider range of section and related structural machines, browse the purlin equipment catalogue. These links are selection routes, not a claim that every illustrated machine has been quoted or tested for your order.
Choose the quoted variant, not only the series name
- F Series FC/FX selectionHistorical HC-300F is C-only; HCZ-300F is C/Z. Check the exact variant, tooling and trial parts in the current proposal.
- N Series NC/NZ/NX selectionHistorical HC-300N is C-only, HZ-350N is Z-only and HCZ-300N is C/Z. For mixed orders, request identified C and Z trial parts and changeover checks in both directions.
Historical names identify questions to ask; they do not confirm current availability, a shared size range or production output.
Calculate changeover value from your own schedule
Record changes per shift, minutes from the last acceptable part of the old section to the first acceptable part of the new section, setup scrap and the cost of stopped production. Compare those records with the quoted equipment and service costs. Without these inputs, no credible payback period can be stated. Ask suppliers to run the same two drawing revisions and material grade so the comparison is fair.
What is included when you buy a purlin machine?
A purlin machine offered for sale is not defined by the main roll former photograph alone. Ask for an itemized supply list that identifies the decoiler, feeding and leveling equipment, punching tools, forming rolls, cut-off, controls, run-out support, guarding, spare parts and services. Mark each item as included, optional or excluded in the specific offer. A current machine photo and trial video should identify the proposed factory and model; they do not replace the signed equipment list.
For a comparable quotation, ask each supplier to price the same approved C and/or Z drawings, steel grade, thickness range, punching layout and target output. Confirm the installation, training, acceptance test and after-sales scope in writing. Halcyon coordinates the proposed configuration directly with the factory production team; the manufacturing entity and the exact equipment are identified in project documents. No stock availability, universal price or delivery date is claimed on this page.
To compare the actual cost rather than an unsupported headline price, use the roll forming machine quotation-scope guide and its buyer worksheet. Record what each offer includes, excludes and requires for acceptance before comparing totals.
When the approved C or Z part is long, specify how the cut section will be supported and removed. Our long-profile runout support guide explains which layout and sample evidence to request; the rating for your line is stated in the quotation.
Inputs to send for a comparable quotation
- Finished sectionsC and/or Z cross-section drawings with revision, flange and lip dimensions
- MaterialSteel grade, thickness range, coating and coil width
- OperationsPunching layout, cut lengths, marking and handling requirements
- Production mixBatch sizes, changes per shift and target output for each section
- AcceptanceSample measurement points, tolerances, test coil and changeover timing definition
Model-specific speed, thickness, accuracy, power and options must be established in the technical proposal and checked at an agreed test. For different section purposes, read C versus Z purlin selection. Halcyon works directly with the factory team on the proposed configuration; the actual manufacturing company and model are identified in project documents.
Buyer selection method: Halcyon Machinery, reviewed 4 October 2026. No customer payback study, universal production speed or acceptance result is claimed here.
Send us your profile drawing
Send both profile drawings and the production mix. We will review the model-specific configuration directly with the factory team.
Get a quoteHow much does a purlin roll forming machine cost?
Direct answer: We quote every purlin roll forming machine by configuration, not from a fixed price list. The price depends on the profile drawing, material thickness, punching and cutting, the level of automation and the delivery terms. Send your drawing and we reply with a written quotation for that exact configuration.
| Configuration level | What changes | Usually chosen for |
|---|---|---|
| Basic fixed-size C or Z line | One section size per tooling setup; sizes changed manually by adjusting or replacing tooling. | Steady orders for one or a few standard sizes |
| Quick-change C/Z line | C and Z sections from one line, with faster shape and size changeover. | Mixed C and Z orders with regular size changes |
| Fully automatic stepless C/Z line | Section width and height set from the control system within the line's size range, with automatic punching and cut-off. | High-mix production and frequent size changes |
Price rises from the first level to the third as tooling, servo control and automation are added.
What affects the price
- Section types (C, Z, sigma or eave strut) and size range
- Steel thickness and yield strength
- Punching layout and cut-off method
- Manual, quick-change or fully automatic size change
- Target output per shift
- Control system and main component brands (PLC, servo, hydraulics)
- Decoiler, outfeed table and automatic stacking
- Delivery terms (FOB or CIF), packing and spare parts
Roll forming machines from Halcyon's Xiamen factory have been used on 150+ construction projects (2022–2026) in China and abroad, including an airport in Iraq, a national stadium in Senegal, resort buildings in the Maldives and a coal preparation plant in Mongolia. See the reference projects.
Evidence to request before approving a C/Z purlin line
Keep the signed drawing revisions, trial-coil identity and the offered tooling list together. Ask us to run the smallest and largest approved C and Z sections, record each adjustment, then check first-off and repeat pieces for section geometry, hole location and cut length. Define changeover time from the last acceptable old-profile part to the first acceptable new-profile part, including setup scrap.
Does an automatic C/Z label prove a fully automatic changeover?
No. The proposal must identify which axes, punching tools, cutters and handling steps change by recipe and which still require an operator. Test C-to-Z and Z-to-C on the quoted configuration.
Which value is the meaningful output target?
Use accepted finished parts for each approved drawing and material under an agreed trial method. Line motion speed alone does not show setup loss, scrap or downstream handling limits.
Which specifications are guaranteed?
Only values written into the machine-specific technical agreement and supported by its acceptance method.
Source: Halcyon Machinery buyer-review checklist, reviewed 4 October 2026.
Material thickness for a purlin machine quotation
State whether the specified thickness is base metal thickness (BMT), the steel substrate thickness, or total coated thickness (TCT), which includes the coating. Supply the steel grade and coating designation with that basis. Do not compare two purlin-machine offers using an unexplained thickness number.
Ask us to state the approved material envelope for each C or Z drawing on the same basis, and identify the actual trial coil. A measurement of a coated strip alone does not establish its substrate thickness or grade.
Material terminology source: BlueScope Technical Bulletin TB-14, BMT and TCT terminology, reviewed 3 October 2026. This reference explains the material terms; it is not a Halcyon machine approval or a finished-building compliance certificate.
Does your schedule include a sloped-flange eave section?
An eave strut drawing may require a separate forming and cut-tool review. Do not assume an ordinary C/Z line covers the required slope, handing, holes and ends. Read the eave strut roof-pitch, handing and cut-tool guide, then send the variant drawings for a configuration review.
Which purlin machine operation manual should the buyer request?
Direct answer: Request the operating and maintenance documentation for the exact machine model, serial number, supplied options and control revision. A generic C/Z selection guide is not an operation manual, and instructions for another variant may not match the installed line. Agree the document language, delivery format and revision with the supplier before acceptance.
Include a document register in the handover scope: operating instructions, the installed-line isolation and safety procedures, the authorized maintenance schedule, component and spare-part identification, electrical and hydraulic drawings where applicable, and the supplier's instructions for the supplied control system. Identify missing documents and responsible contacts; a catalogue photograph or a sample recipe does not replace them.
Where software or control files are included, confirm separately which backups, licenses, passwords, restore instructions and support rights are delivered. File ownership or possession alone does not establish permission to edit controls or compatibility with a replacement controller. Use the PLC backup and handover guide to record agreed scope, and the machine-specific maintenance record guide to organise authorized tasks.
For an existing machine, send the model and serial number, manual revision, control identification and the document or support question to the authorized supplier. Do not start or adjust a machine using this procurement checklist. Include documentation and training requirements with your C/Z inquiry.
Procurement documentation checklist reviewed 5 October 2026. No downloadable model-specific operation manual, universal operating sequence or guaranteed training package is claimed here.