
Identify the roof profile
Mark rib height, pitch, pan width and the edge that forms the side lap on the approved drawing.
Compare roof sheet roll forming equipment against your panel drawing, effective cover width, material and trial sample. The quoted configuration is confirmed after a drawing and production review.
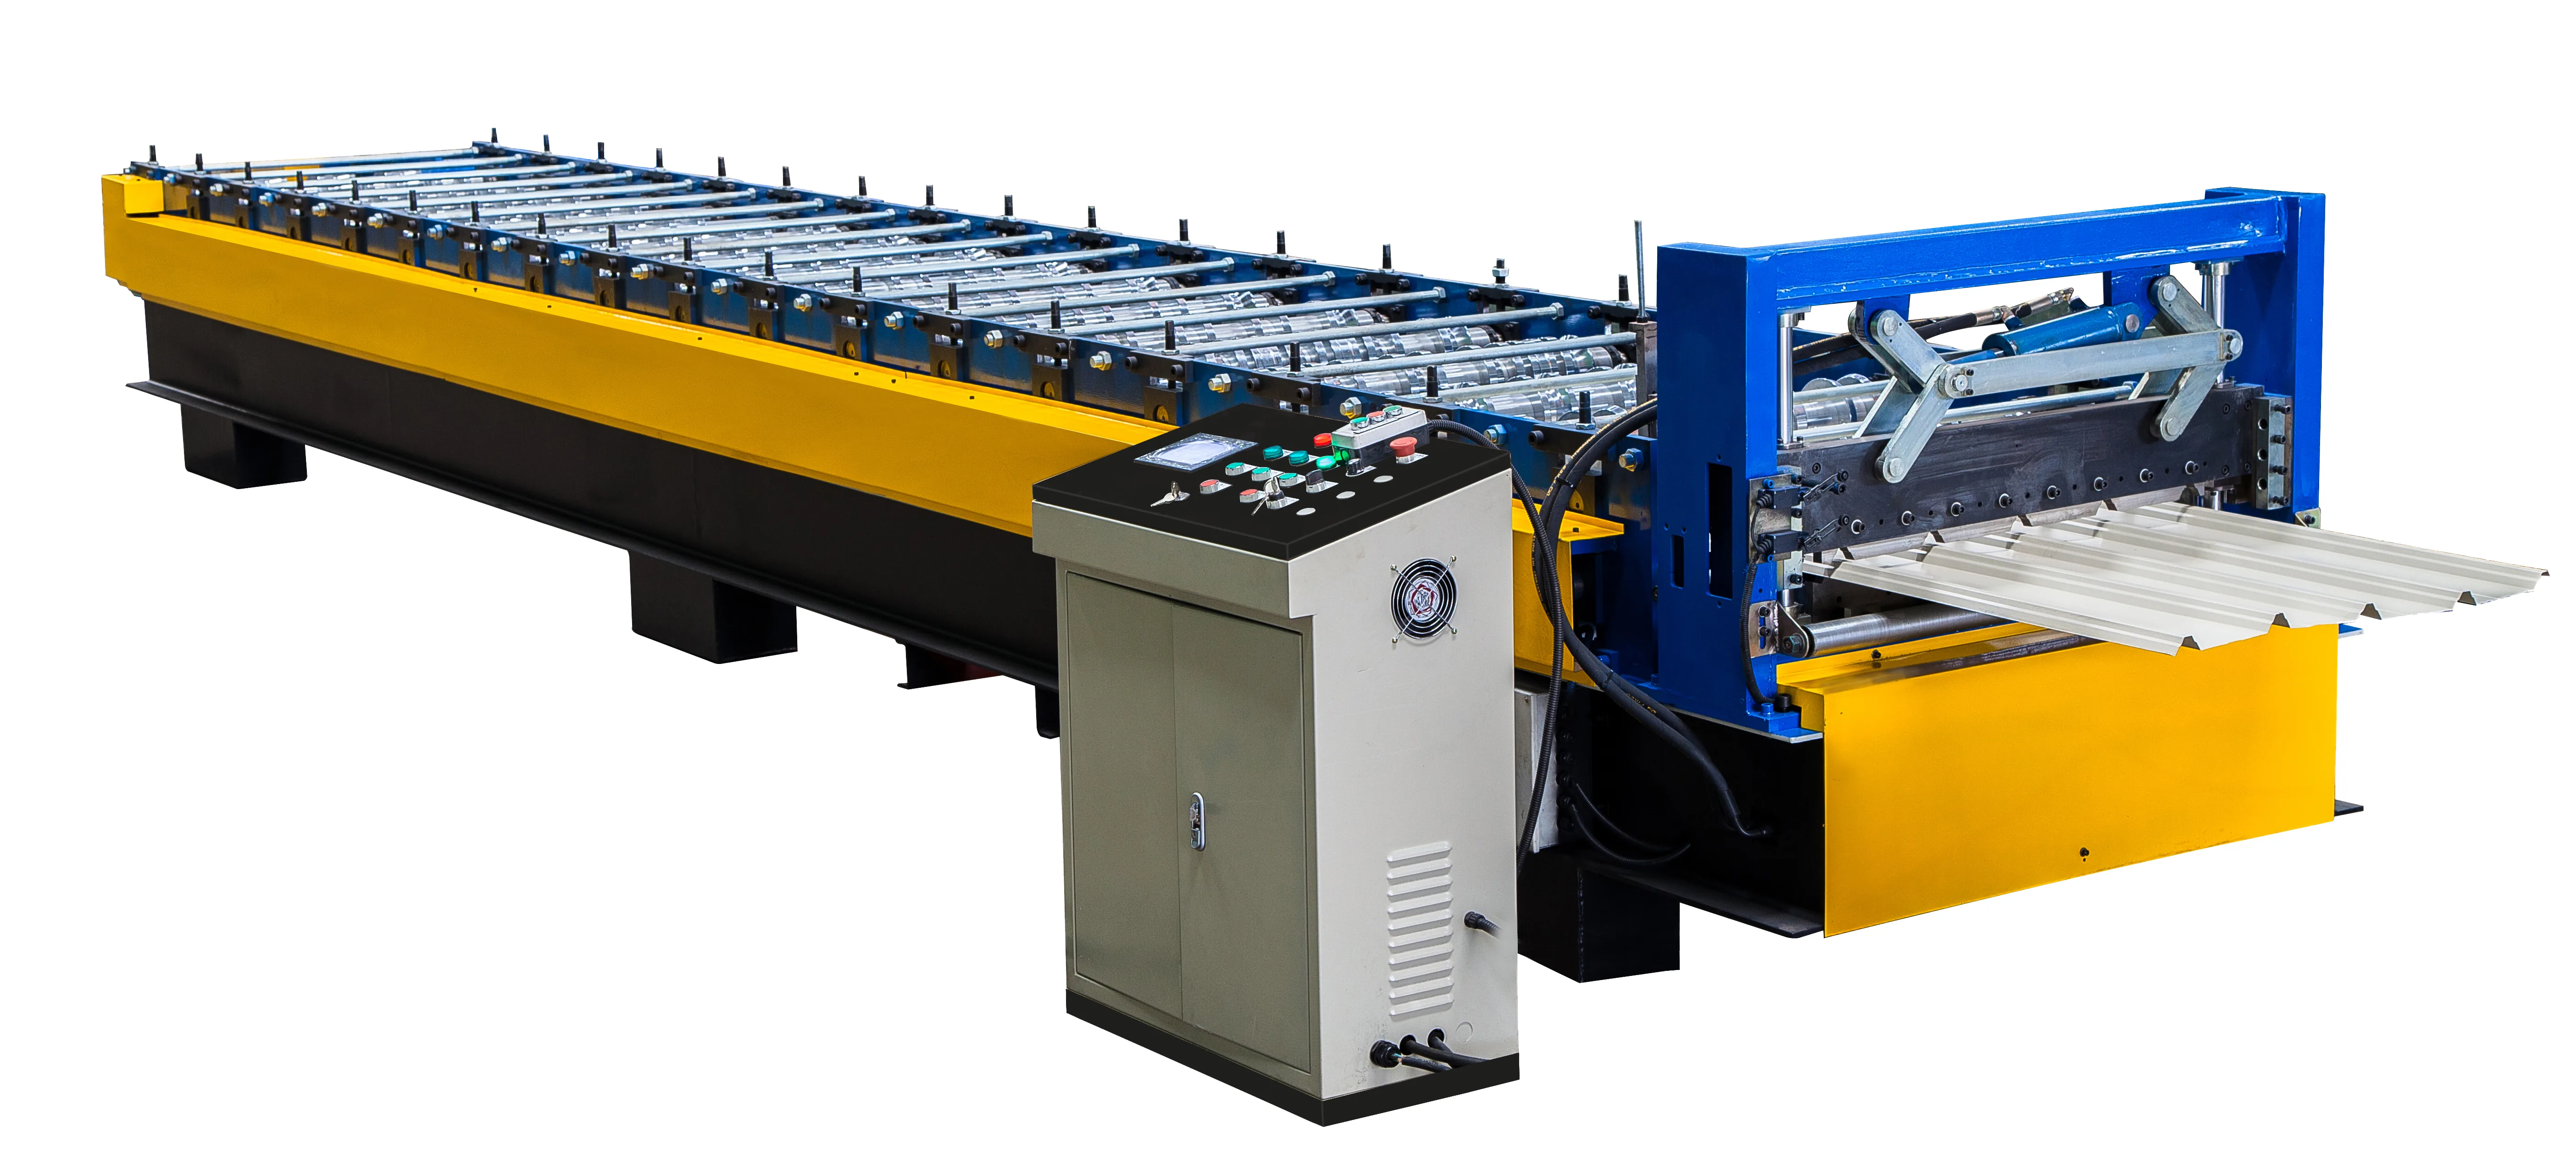
production-base equipment photo showing one profiled panel at the run-out. This is an example line, not the quoted machine or proof of the requested cover width, speed or acceptance. Confirm the proposed profile and sample against your drawing. View the full-resolution reference photo.
Direct answer: A “roof sheet making machine” listing names the equipment category, not a proven match to your roof panel. Send a dimensioned drawing showing rib height, pitch, overlap edge and effective cover width; then compare an identified trial sheet against that same drawing.
Mark rib height, pitch, pan width and the edge that forms the side lap on the approved drawing.
State steel grade, base-metal thickness, coating and coil width so the proposed tooling and trial use the same material basis.
Join two identified trial sheets in the intended direction and measure effective cover width separately from overall sheet width.
Check first-off and repeat sheets for coating contact marks, edge condition and the agreed finished length. For prepainted coil, use identified trial material and inspect guide, forming, cut-off and outfeed contact points; the surface-quality buyer guide lists the evidence to record.
Values below separate confirmed product information from project-dependent engineering data.
Reference-data rule: this page contains selection questions rather than model-specific performance figures. Power, speed, tooling, dimensions and guaranteed accuracy become binding only when repeated in the signed technical agreement for your project.
The proposal defines every station, interface, production assumption and acceptance checkpoint.
Trapezoidal, corrugated and standing-seam panels are different profile families. Compare quotations only after identifying the intended panel drawing and its installation overlap.
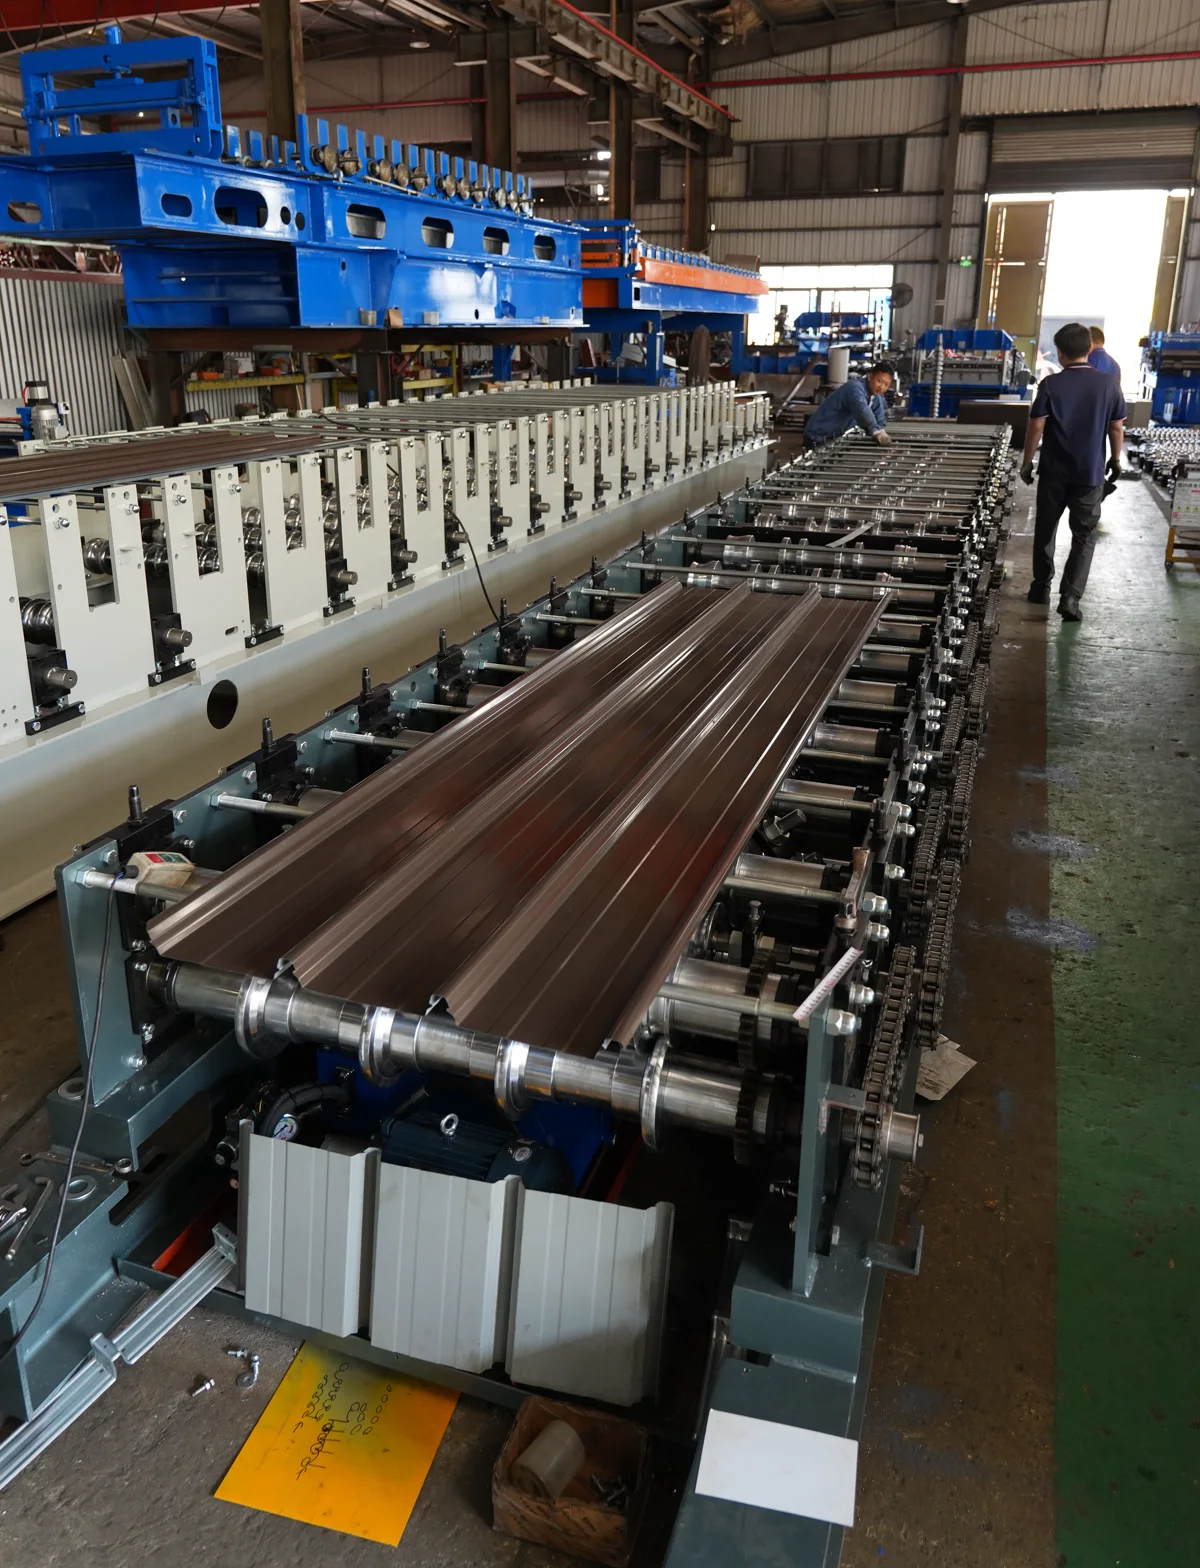
In this 27-second production-base workshop clip, the camera follows a formed roof panel and shows roller contact areas. Use it to ask for the approved panel drawing, trial coil record and visible surface checks. The clip does not identify the offered machine configuration, establish production speed, certify coating quality or replace measured sample acceptance. English narration and synchronized visible English captions are included.
Video source: Halcyon Machinery's production-base workshop clip, published 25 September 2026. The separate Xiamen trial-sheet photograph above is not claimed to show this same line. AI English narration is disclosed on the video.
Options are quoted only when they match the approved production workflow.
Confirm the proposed decoiler, guides and contact points against the stated coil weight, coating and surface requirements.
Identify whether the quotation covers the approved trapezoidal, corrugated or other drawing; a family name does not include every toolset.
Record the intended overlap direction and the trial method for measuring effective installed cover width.
Specify finished lengths, cut-edge checks and any drawing-dependent end cuts before selecting the cutting arrangement.
Agree how trial sheets are supported, collected and inspected without damaging the stated surface finish.
List the drawing revision, coil identity, measured first-off and repeat sheets, and acceptance record in the offer.
Trapezoidal, corrugated and wall-cladding panels for building envelopes. Buying your first line? Read how to choose and buy a metal roofing machine.
Send the approved panel cross-section showing rib height and pitch, both side-lap edges, overall sheet width and intended effective cover width. Add the coated-coil grade, base-metal thickness, finish and cut-length schedule. The tooling and trial must be checked against that exact drawing.
Do not assume so from a generic line photo or model name. These are different profile drawings. Ask our factory team to identify and quote the tooling, adjustments and trial sheets required for each proposed panel family.
List the included decoiler, guides, forming tools, cut-off, run-out and handling scope, with the stated coil and operating conditions. Measure identified trial sheets against the approved drawing, join two in the intended overlap direction, and check effective cover width, surface condition and finished length before acceptance.
Direct answer: The buyer should check a pair of identified trial sheets joined in the drawing's specified overlap direction. Measure the finished sheet width and the effective installed cover width separately, at agreed datums, then compare the assembled joint, ribs and cut length with the approved profile drawing. A single unjoined sheet cannot prove the coverage of the installed roof.
| Check | Record from the trial | Why the buyer needs it |
|---|---|---|
| Drawing and coil | Drawing revision, steel grade, coating, thickness and coil width | Connects the sample to the proposed tooling and material range |
| Sheet geometry | Rib height and pitch, pan width, edge geometry and finished length | Checks whether the produced panel matches the ordered section |
| Installed coverage | Two-sheet side lap, overlap direction and measured effective cover | Separates sheet width from the roof area covered after assembly |
| Surface and repetition | First-off and repeat samples, coating contact marks and cut edge | Shows whether the result is repeatable on the specified material |
Terminology: Buyers may search for a “roof sheet roll forming machine,” “metal roof panel machine” or “roof panel roll former.” These terms refer to equipment procurement here, not the purchase of finished roofing sheets. A corrugated, trapezoidal or concealed-fix drawing needs its own tool and joint review; do not infer that one quoted line makes all three. If your project needs both roof and wall cladding profiles, see the roof and wall sheet line scope to define each drawing and trial sample before comparing tooling.
Searches for a “metal roofing machine for sale” can include both factory-installed panel production lines and portable job-site roll formers. This page covers a factory production-line proposal matched to a roof-panel drawing. If you need a trailer-mounted or on-site machine instead, say so in the enquiry; portability is not implied by the catalogue photo or by the words “roofing machine.” Use the factory-versus-portable comparison to check which production route fits your site before asking for a quote.
For a comparable factory-line quotation, identify the panel drawing and intended overlap, coil grade and thickness, required punching or end-cut layout, target output, site power supply and the handling or stacking scope. Ask each supplier to mark included modules and exclusions against the same drawing before comparing offers. A price or delivery date cannot be inferred from a generic machine name.
Source and limit: LYSAGHT's roofing guide explains why sheet width and effective cover differ with side overlap. The acceptance steps and roof-sheet-specific buyer questions above are Halcyon Machinery's buyer-review method, updated 2 October 2026; they are not measured results for a named machine. Use the full roof-sheet lap trial guide for the recording method.
Direct answer: We quote every roof sheet roll forming machine by configuration, not from a fixed price list. The price depends on the profile drawing, material thickness, punching and cutting, the level of automation and the delivery terms. Send your drawing and we reply with a written quotation for that exact configuration.
| Configuration level | What changes | Usually chosen for |
|---|---|---|
| Single-profile line | One panel profile with post-cutting and manual run-out. | One standard roof or wall profile |
| Double-layer or multi-profile line | Two panel profiles on one machine, or exchangeable tooling. | Buyers who sell two common profiles |
| Automatic line with stacking | Automatic cut-to-length, run-out and stacking for higher daily volume. | Continuous production for distributors and contractors |
Price rises from the first level to the third as tooling, servo control and automation are added.
Roll forming machines from Halcyon's Xiamen factory have been used on 150+ construction projects (2022–2026) in China and abroad, including an airport in Iraq, a national stadium in Senegal, resort buildings in the Maldives and a coal preparation plant in Mongolia. See the reference projects.
Compare quotations for the same panel drawing, coated coil and finished-length schedule. Ask the supplier to itemize the forming tools, coil handling, cut-off and sheet collection rather than comparing an unexplained machine total. Halcyon reviews the profile, coil and complete equipment scope before quotation. Price and delivery must be confirmed for that configuration.
Request an offer showing inclusions, exclusions, currency, validity and delivery basis. These fields must be confirmed for the actual project; a catalogue photograph cannot establish the delivered scope. Use the itemized quotation comparison guide to keep supplier offers comparable, then send your panel drawing and production schedule. Trial-sheet acceptance remains separate from the roof designer's checks on the complete installed roof system.
We will review the model-specific configuration directly with the factory production team and identify which values need a trial or technical agreement.
Specify the thickness basis with the coated-coil details. Base metal thickness (BMT) describes the steel substrate; total coated thickness (TCT) includes the coating. These figures are not interchangeable when comparing machine proposals or the panel drawing.
For the trial, record coil identity, grade, coating and the agreed thickness basis. Ask our factory team to confirm the tooling and material envelope for that coil, then inspect the formed sheet and side lap. Do not derive substrate thickness from an unspecified coated-sheet measurement.
Material terminology source: BlueScope Technical Bulletin TB-14, BMT and TCT terminology, reviewed 3 October 2026. This reference explains the material terms; it is not a Halcyon machine approval or a finished-building compliance certificate.