
LA Hat Profile Roll Forming Machine: HHP-30 Buyer Review
Our Xiamen production base publishes HHP-30 as a hat-profile line, including inclined-web variants. Send the exact section and material before treating another hat or omega drawing as compatible with the quoted tooling.
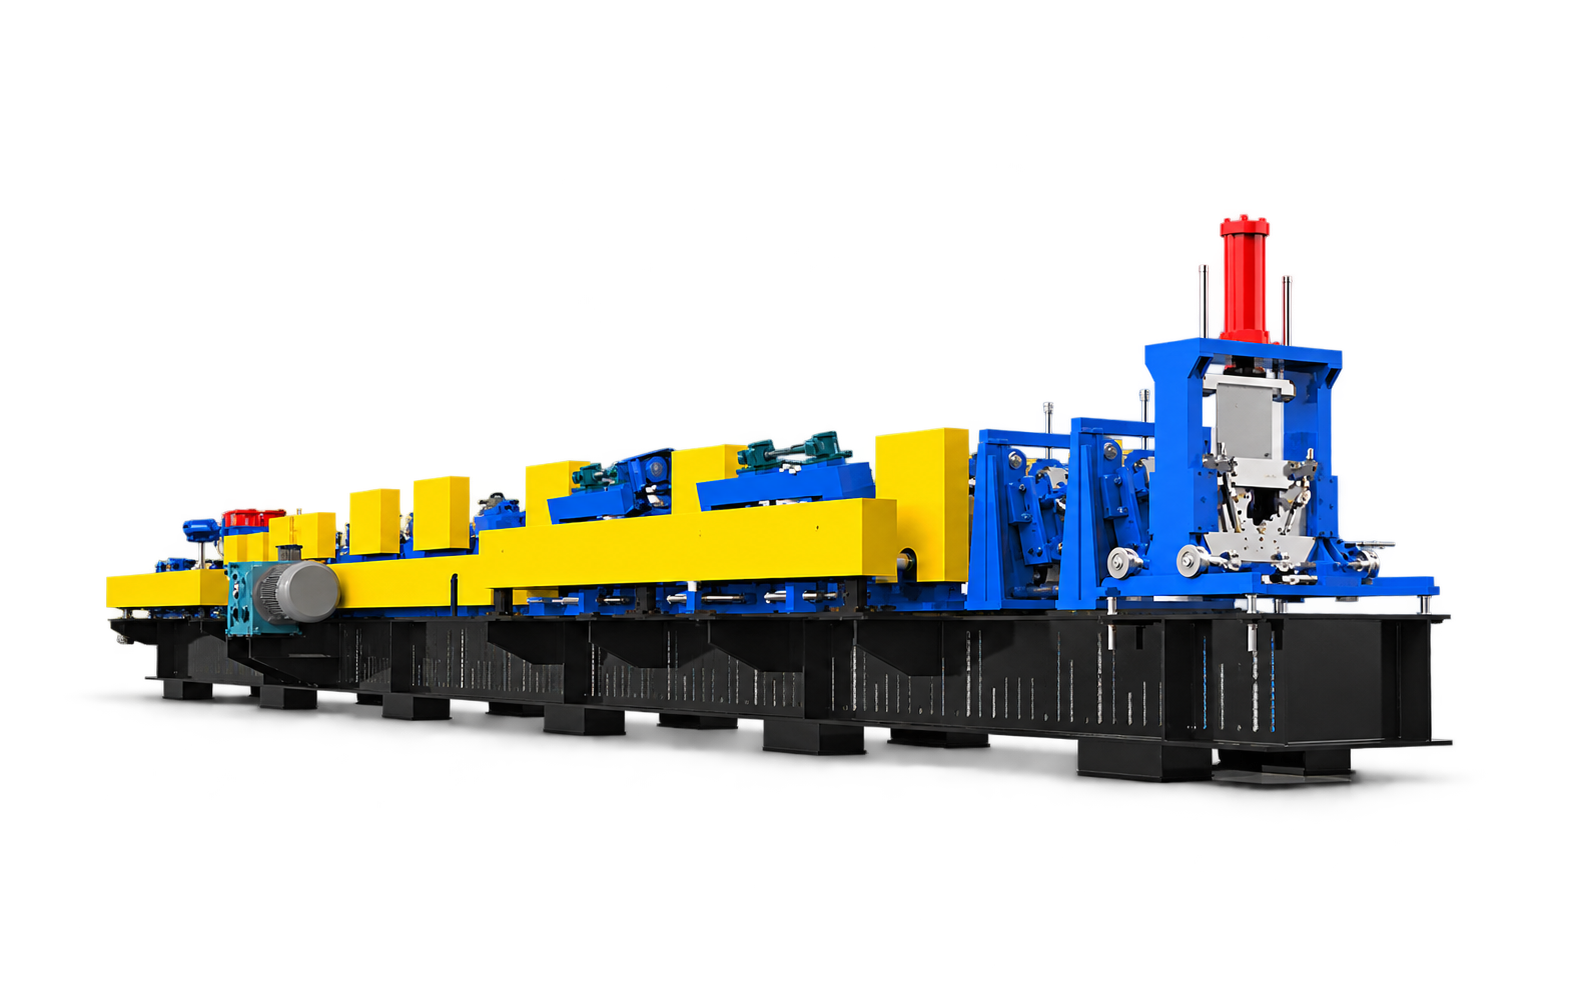
Production-base rendering. Request current build photos and the proposed line layout.
Can the LA line make your hat or omega section?
Use our Xiamen production base's HHP-30 page as a starting reference for a hat section, not as proof that the same roll set makes every omega profile. Compare the approved base, web angle, crown, flange, return lip, material and holes against the proposed tooling drawing. A similar-looking section can require different rolls, guides, punches or cutter tools. Ask our factory team to confirm the exact profile family and changeover work in writing before ordering.
For an omega or ceiling-furring section, send a separate drawing and intended assembly. The visible supplier reference identifies a hat machine; it does not establish a universal omega capability. Use the omega furring buyer checklist to record the separate geometry, fixing and sample-fit requirements.
What the HHP-30 source actually specifies
These are production-base catalogue figures for its named example. They are not Halcyon-owned test results or guaranteed values for your order.
- Production-base example
- HHP-30 hat-profile roll forming machine
- Published material
- Hot-rolled strip or hot-dip galvanized strip; confirm the order grade and coating
- Published thickness range
- 0.8–2.0 mm in the production-base reference; verify the exact grade and section at quotation
- Published forming stations
- 16 for the named reference; final tooling and station arrangement require the offered layout
- Published speed distinction
- 28 m/min forming reference versus 12–18 m/min stated overall with punching dependency; neither is a guaranteed output for a new drawing
- Punching and cut-off
- Supplier page describes post operations, while its flow chart is shorter; request a station-by-station drawing and trial sequence
Our Xiamen production base's narrative and table do not use identical wording for every profile dimension and station. Do not transfer catalogue figures to a different section. Read our Xiamen production base's HHP-30 reference.
Compare the drawing with the proposed tooling
Provide the steel grade, thickness range, coil width, finished lengths, hole positions and target output. For mixed hat and omega orders, ask which rolls, guides, dies, cutter tools and settings change, then compare first-off samples from each requested profile. A controller recipe alone does not prove a physical tooling changeover is possible.
Reference image versus the machine offered
Our Xiamen production base also publishes an original HHP-30 workshop photograph. It shows a machine in our Xiamen production base; it is not a photo of the specific line offered in a Halcyon quotation. Request dated photographs or video showing the selected line, plus a layout and identified profile samples for the actual offer.
Check useful output, not catalogue line speed alone
- Agree the drawing revision, steel batch, thickness and hole schedule used in the test.
- Measure base, web angle, height, flanges, lips, hole positions and cut length on first-off and later pieces.
- Record forming speed separately from complete-line output with the specified punching and cutting pattern.
- For a proposed second profile, retain labeled samples and record each tooling or guide change and setup time.
- Check fit in the intended supporting assembly; a dimensional sample alone does not prove structural capacity or building-code compliance.
Related decisions: custom steel-section buyer review and FAT evidence checklist.
Questions to settle before quotation
Does HHP-30 also make omega sections?
The published HHP-30 example is a hat-profile machine. Omega production is not established by that page; submit an omega drawing for tooling review and sample evidence. Use the omega-profile drawing and inspection guide to define the checks before quotation.
Can I use our Xiamen production base's 28 m/min figure as my output target?
No. That is a catalogue forming-speed reference. The same source gives a lower overall range affected by punching; agree a measured complete-line trial for your profile and hole pattern.
What should the quotation name?
The exact model or custom configuration; approved drawings; material; tooling, punching, cut-off and handling scope; trial material; sampling method; exclusions and responsibility for acceptance.
Source and review: HHP-30 product page, checked 24 September 2026; Halcyon Machinery buyer-review framework, updated 24 September 2026. No customer installation, universal omega capability or guaranteed speed is claimed.
Send the hat or omega drawing for a tooling review
We will ask our factory team to identify the configuration and evidence for your actual section before confirming scope.
- Dimensioned section and intended application
- Steel grade, coating and thickness range
- Punching layout and cut lengths
- Profile mix and target output per shift
- Destination electrical supply