
By Halcyon Machinery · Published
Specify and inspect strip-entry guides on a roll-forming line. Compare coil condition, guide settings and first-off parts before approving a machine trial.
Direct buyer answer
Ask for an adjustable, documented entry setup and prove it on finished parts made from the specified coil. An entry guide helps bring strip into the first forming pass in a repeatable position. A photograph of the guide, or a centered strip at one moment, cannot establish that tracking stays stable through production. Agree the coil, profile drawing, guide-setting method and part-inspection points with our factory team, then record first-off and repeat samples.
Separate incoming-coil condition from line adjustment
Record the coil ID, steel grade, coating, thickness range and slit width before changing a guide. Inspect the incoming strip for edge damage and visible sideways curvature. Incoming camber can make the strip track differently even if the entry guide position has not changed. Do not promise that guide adjustment alone will correct a bad coil. Metform's published technical FAQ distinguishes incoming camber from sweep in a formed part; use the quoted machine's own documented settings for the actual trial.
| Buyer check | Evidence to retain | What it does not prove |
|---|---|---|
| Entry-guide scope | Proposed guide type, adjustment range, side-setting method and quoted drawing | That every coil width or profile has been tested |
| Trial material | Identified coil, grade, thickness, width and visible edge condition | That a different coil will track the same way |
| Setup repeatability | Recorded inboard/outboard or equivalent guide settings for each trial | That a dial position alone meets part tolerances |
| Finished profile | First-off and later samples measured from agreed datums | That a still photo demonstrates sustained production output |
Samco describes individual side settings as a way to make strip position in the roll tooling repeatable. That is a useful procurement question, not a claim that every proposed line includes digital readouts. Ask our factory team which adjustment and recording method is actually included.
Run a practical acceptance check
- Send the revision-controlled profile drawing, with datums and agreed cross-section, straightness and cut-length inspection points.
- State the steel grade and thickness range, coating, slit width and coil condition. Use identified trial stock that matches the quotation.
- Include the punching layout if hole positions depend on strip tracking; compare holes on finished parts, not only the flat feed.
- State the target output and the run duration to be demonstrated, without treating the supplier's advertised speed as measured performance.
- Record the entry-guide setting, take a labelled first-off piece, run the agreed sequence and measure later samples. Repeat after a change of coil width or profile only if that change is part of the purchased scope.
If parts drift or the guide needs constant manual correction, pause the acceptance decision and ask our factory team to distinguish coil camber, guide setup and forming-tool alignment. The responsible engineer should define pass/fail limits from the buyer's drawing; this article does not invent a universal tolerance.
Buyer questions
Does an entry guide fix every curved or twisted profile? No. Incoming coil shape and forming pressure also matter. Diagnose the source using identified material and measured finished parts.
Should I require digital readouts? Ask how the quoted guide settings will be recorded and repeated. Digital readouts are one possible method described by Samco, not a universal requirement or an included Halcyon specification.
Can a single trial prove all coil widths and profiles? No. Define representative changeovers from the actual purchase scope and retain separate samples for each agreed configuration.
Sources, limits and enquiry
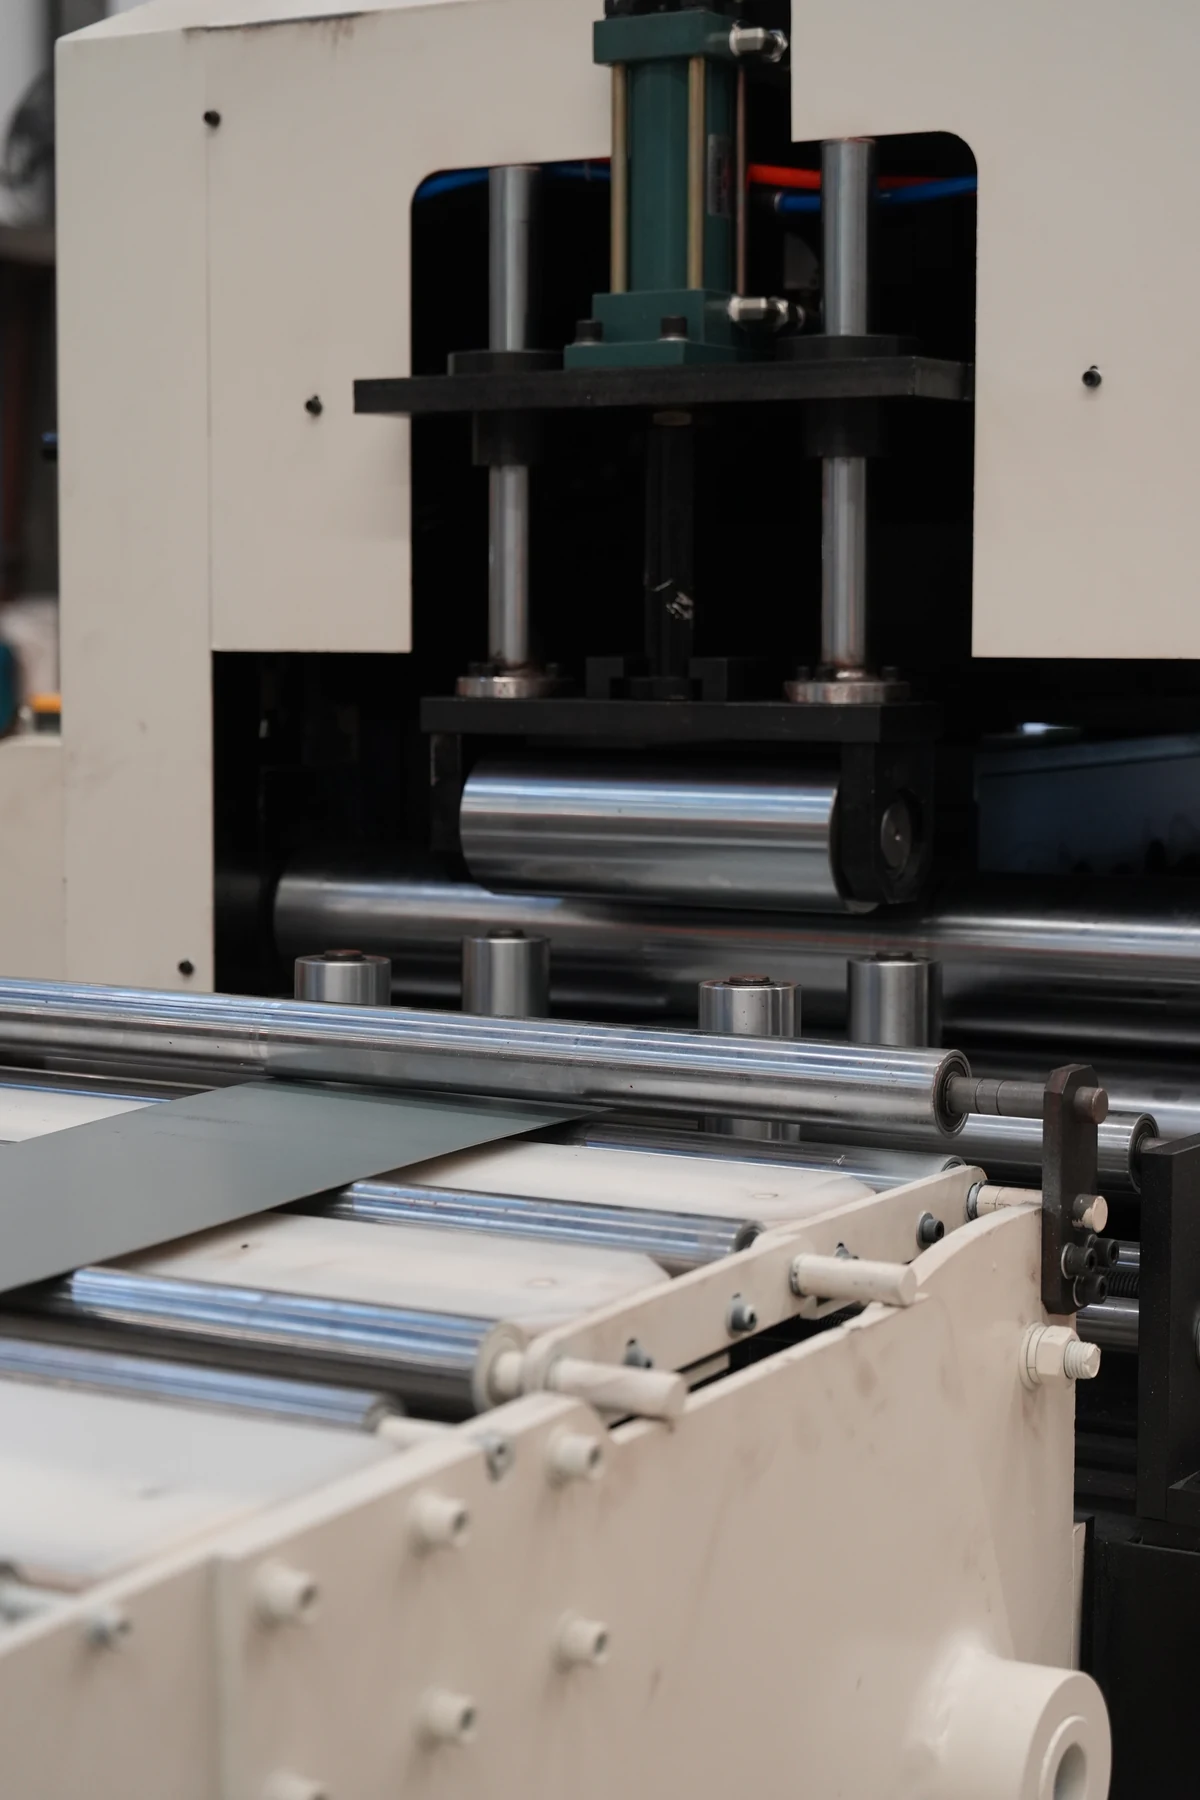
Technical context: Samco Machinery's entry-guide discussion and Metform's line-equipment and defect FAQs, linked above. The accompanying image is a site-visit illustration of strip between lateral guide rollers, not proof of an approved setting, a customer case, a named model or an acceptance record. Halcyon Machinery handles equipment specification and supply factory-direct from our Xiamen production base. Our factory team must identify the actual guide and demonstrate its performance.
Review decoiler and entry equipment, C/Z machine selection, roof-panel equipment and the finished-part sample checklist. Send the profile drawing and coil details for a supplier-specific review.
Technical sources for review
- Samco Machinery: entry-guide side settings
- Metform: material handling and entry table
- Metform: incoming camber and formed-part sweep
These sources provide general technical context, not proof of the configuration or acceptance result of a machine quoted by Halcyon.